Solution 02
Machine vision & quality control
Inspection, detection, sorting and traceability defined from real defects, product references and reject criteria agreed with the site team.
Describe the need → SYNTAVER · Machine vision & quality control
When this solution makes sense
Signals we look for on site.
We engineer the complete inspection system, not only the camera, to secure repeatability, maintainability and useful defect interpretation.
Subjective or costly manual inspection
Operator variability, visual fatigue or inspection cost increasing with throughput.
Presence / absence / orientation defects
Presence, absence, orientation, assembly or appearance defects to check repeatably.
1D/2D code reading and traceability
Codes, lots or serial numbers to read and associate with the production cycle.
Automatic product sorting
Need to separate conforming / non-conforming product with controlled reject logic.
Need for in-process quality evidence
Images, results or statistics required for quality analysis and reject traceability.
Typical scope
What the project can include.
Vision feasibility study
Camera, optics and lighting selection
Station design and product presentation
Inspection algorithm and recipes
PLC interface, rejection and traceability
Validation on representative samples
Technical depth
Open the technical layer that matches your question
These items do not replace a site survey; they show the level of detail used to scope a pre-study.
01Data to collect+
- Representative good / bad samples
- Defect size and contrast
- Throughput, product speed and available distance
- Colour, position and ambient light variations
02Possible building blocks+
- 2D / 3D camera depending on application
- Dedicated optics and lighting
- Triggering, tracking and reject
- PLC / database / traceability
03Useful deliverables+
- Defect matrix
- Vision feasibility report
- Integration diagram and reject logic
- Test plan with representative samples
04Acceptance criteria+
- Defined defects detected
- False rejects / false accepts measured
- Processing time compatible with line speed
- Recipes, maintenance access and diagnostics
Method
Three scoping steps before integration.
The objective is to reduce grey zones before placing orders or starting on-site work.
1. Gather defect references
Samples, product variability, lighting conditions and line speed.
2. Define the inspection logic
Presence, conformity, sorting, OCR or measurement depending on the real need.
3. Validate at production speed
Trials, detection rate, false rejects and operator interface.
Related use case
Modernising a sorting and quality-control station
See how this type of need can be scoped, structured and measured.
View the scoping →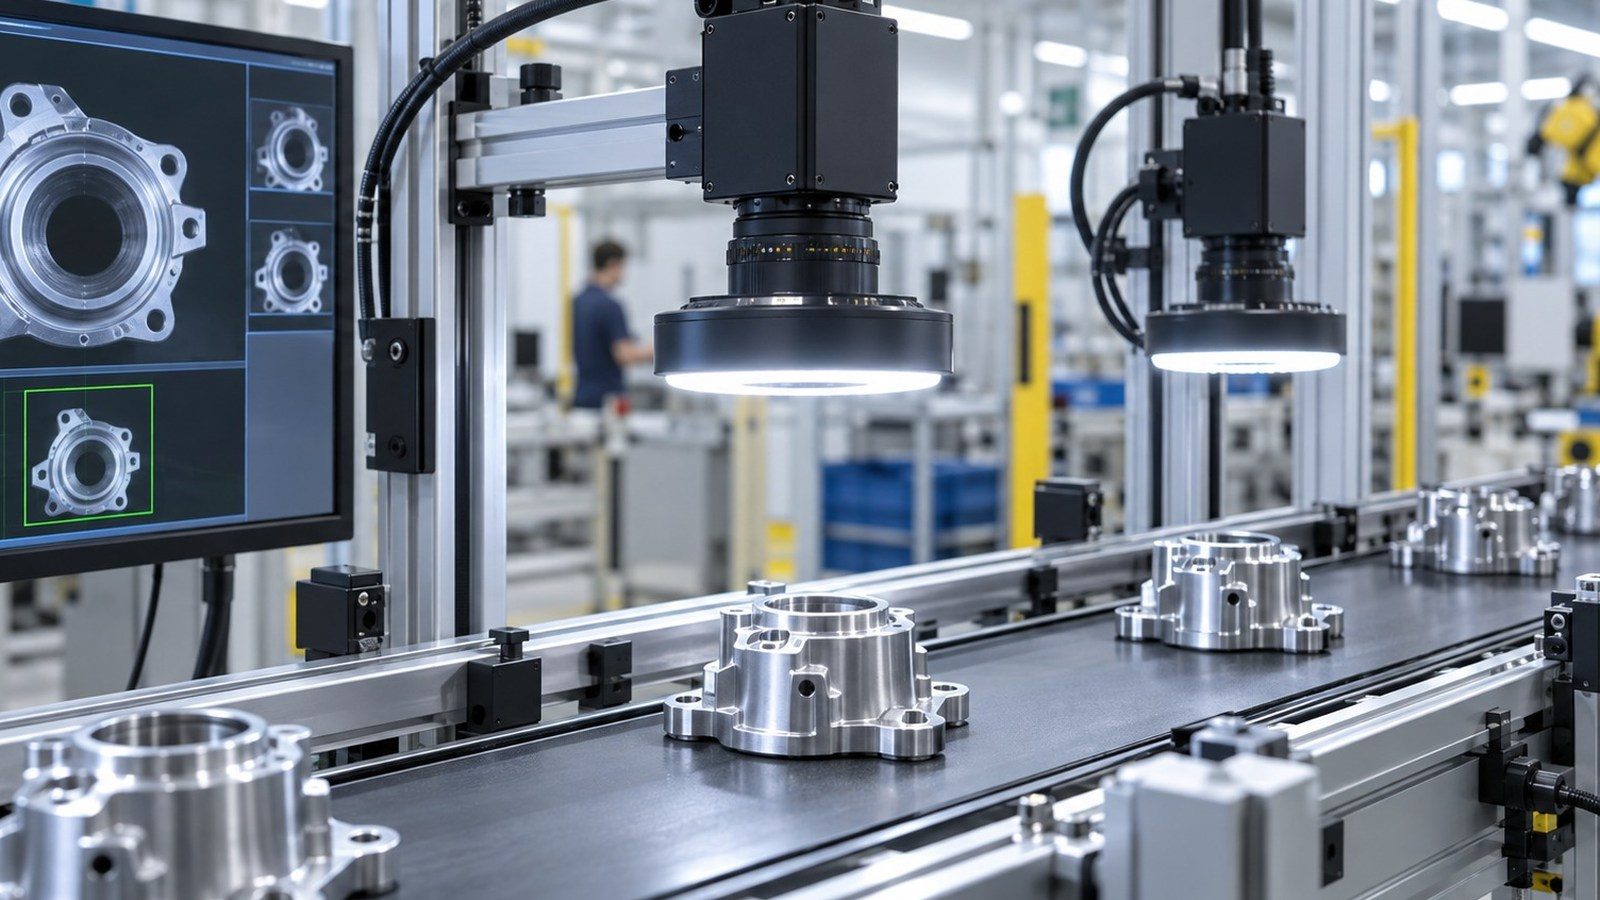
Next step